A marine fender pad is normally bought as an accessory and specified as an afterthought. That one habit causes most of the berth protection problems we get called about. The pad is the only part of the fender system that actually touches the hull: it sets the friction the vessel slides against, it spreads reaction force into the rubber, and it carries every bolt load into the panel behind it. Choose it by vessel tonnage or by whatever the last project used, and the system still works, just badly.
This guide covers the four decisions that change field performance: thickness, molecular weight grade, colour and UV package, and the fixing detail.
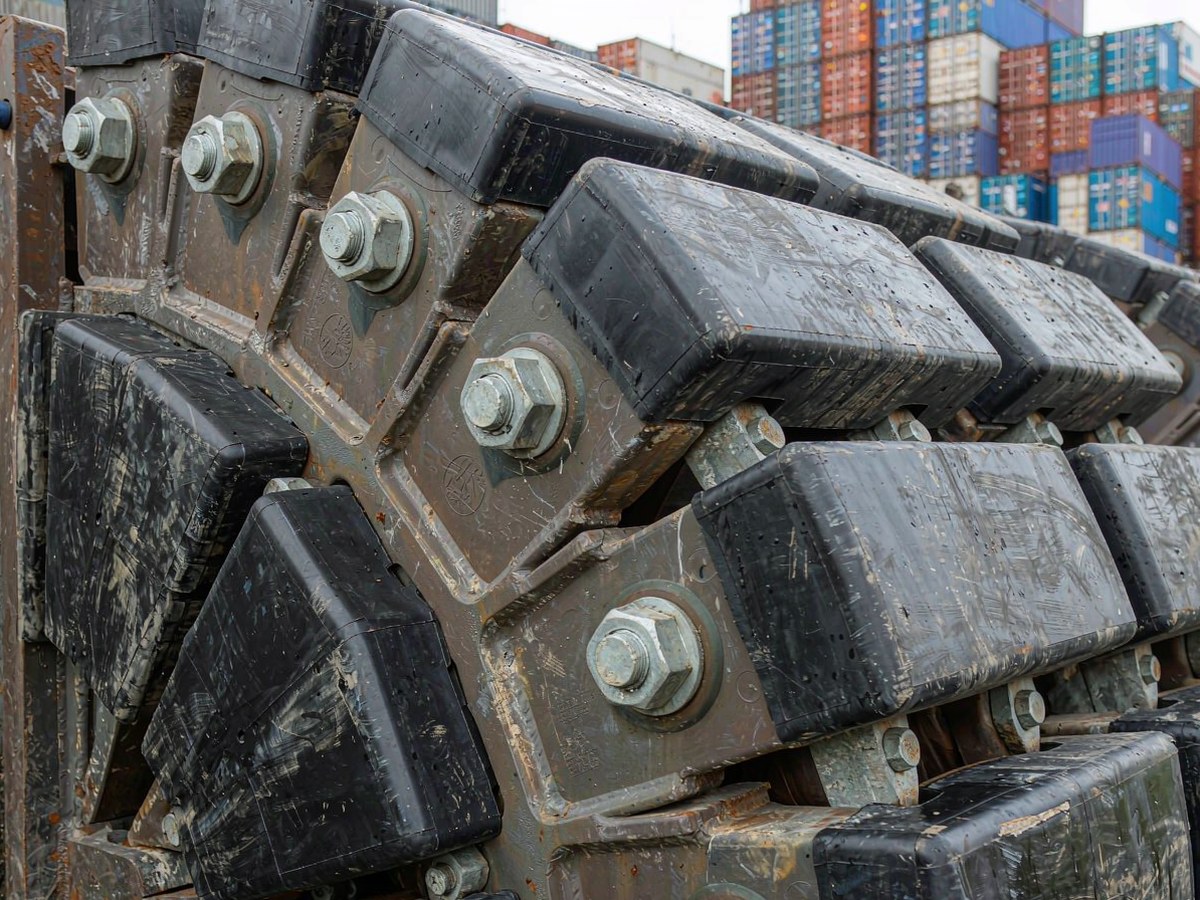
Berthing energy is absorbed by the rubber element and by the deflection designed into it. The steel panel transmits reaction into the quay. The pad does none of that work. Its job is to present a low friction, abrasion resistant face so the hull slides along the fender instead of dragging across it, and so the rubber never contacts a painted hull directly.
That distinction has a practical consequence: a thicker marine fender pad does not give you more energy absorption, and it will not rescue an undersized fender. What extra thickness buys is wear allowance, bolt embedment depth, and enough material to spread contact pressure without cold flowing around the fasteners. If the berthing energy calculation is short, no facing material fixes it.
Friction governs the rest. Dry UHMWPE against painted steel sits around 0.1 to 0.2 coefficient of friction, roughly a fifth of what rubber on steel gives you. In a silty or sandy berth the grit film between pad and hull raises that number and turns the pad into a wear part rather than a sliding surface, which is why abrasion resistance of the grade matters more than its quoted impact strength.
Sizing a marine fender pad from vessel tonnage alone is the usual mistake. Size only matters through contact pressure and berthing frequency. A 30 mm pad under a 5,000 DWT coaster berthing twice a week is a different proposition from the same pad under a panamax box ship with a tug pressed against it for twenty minutes.
The market has settled into bands most specifiers work from. Pads of 20 to 30 mm suit marinas, small craft berths, pilot boat landings and low energy faces where the vessel is essentially stationary on contact. The 40 to 50 mm band is the working standard for general cargo and multipurpose berths. The 60 to 80 mm band belongs on container terminals, bulk export berths and RoRo ramps that see high contact pressure, tug assistance or frequent heavy sliding. Above 80 mm you are into oil and gas terminals, very large vessel berths and lock entrances where a barge may nose in at an angle.
Treat those bands as a starting point, then check two numbers with the supplier. First, the allowable sustained contact pressure at your design temperature, because polyethylene creeps under steady load and a pad held in compression for years will thin and dish whatever the room temperature datasheet says. Second, the wear allowance over the inspection interval you actually intend to keep. If the terminal inspects every five years, the pad needs enough sacrificial thickness that five years of grit abrasion does not expose the steel panel.
Thickness tolerance matters as much as nominal thickness. Pads bolted in a field across one fender face must sit at consistent height, otherwise the proudest pad takes the whole load and fails first. Call out a flatness figure and a tolerance band on the drawing, not just a nominal dimension.
Marine pads are normally cut from resin in the 3 to 9 million g/mol range. Below roughly 3 million you are into high molecular weight material with noticeably lower abrasion resistance and impact strength. Above 9 million, machining becomes difficult and the wear gain flattens out. Most berth work lands between 3 and 6 million, with the top of that range reserved for heavy sliding contact and grit-loaded water.
The commercial labels on quotations, PE 500, PE 1000, UHMW 1000, mean very little on their own. They are supplier shorthand, not standardised designations, and they vary between producers. What you can verify is a molecular weight test report from the resin batch, a density figure in the 0.93 to 0.94 g/cm3 range, and abrasion data from a named test method. Ask for those three and you will find out quickly whether the quote is genuine UHMWPE or HDPE wearing the right words.
Reprocessed UHMWPE is cheaper and not automatically unsuitable. For a low energy face, a non-critical rubbing strip or a temporary berth, well sorted reprocessed sheet is a reasonable commercial choice. The problem is batch variation in molecular weight and contamination, and contamination is what starts edge cracks and tear propagation in a marine facing.
For a permanent berth with a twenty year design life, specify virgin resin and put the wording in the purchase order. The premium on a 50 mm pad is small against a fender change out, which means crane time, divers or a work boat, and a berth out of service for a week. The economics only look close if you compare material price per square metre and ignore everything after installation.
Black is the default because carbon black is the most effective and cheapest UV stabiliser available for polyethylene. A black pad in a tropical berth holds its mechanical properties far longer than an unstabilised natural coloured one, which will chalk, micro-crack and lose surface toughness in direct sun.
Coloured pads, yellow, blue, red, orange, are used for visibility: marking a berthing line, flagging a replaced fender, or making a low pad visible to a mooring crew. That is a legitimate reason to pay more, but only if the colour compound carries a UV stabiliser package. Ask what stabiliser system is in the material, not just what colour it is. A bright yellow pad with no UV package is a two year product in strong sunlight.
Most marine pad failures we see start at a hole. Get the pattern right at the drawing stage and half the risk disappears before anything is fabricated. The first rule is to drill from a template taken off the actual fender panel, not from a catalogue drawing. Hole spacing on cone and cell fenders is not identical between manufacturers, and a 10 mm mismatch becomes an oversized hole, a loose pad and a crack initiation site.
The second rule is countersinking. Bolt heads must sit flush or below the pad surface. A protruding head catches the hull, tears paint and can be ripped out of the pad entirely during a hard contact. Specify countersunk or recessed heads with a chamfer that removes the sharp edge where stress concentrates.
The third rule is slots rather than round holes where movement is expected. A slotted hole with a washer plate lets the pad expand and contract without loading the fastener in shear. The fourth is edge treatment: a chamfered or radiused edge resists chipping far better than a sawn square edge. Thickness tolerance, flatness and hole position tolerance should all be on the drawing. Suppliers hold them if you ask; they will not guess what you meant.
UHMWPE moves. Its coefficient of linear expansion is in the region of 1.5 to 2.0 x 10^-4 per kelvin, roughly fifteen to twenty times that of steel. On a 1,000 mm pad seeing a forty degree swing between a cold night and afternoon sun on a dark surface, that is six to eight millimetres. Constrain that with fully tightened bolts in round holes and something has to give, and it will be the pad.
Design the fixing as a set of clamped points rather than a rigid frame. Use oversized or slotted holes with clearance calculated from panel length and local temperature range, use washers large enough to spread the clamping load, and do not over-torque. Over-tightening is the most common installation error on these pads: it crushes the material around the hole, creates a hard spot, and starts a crack that runs across the face within a season.
Stainless fasteners are standard in a salt atmosphere, and where the panel is carbon steel an insulating washer between fastener and panel reduces galvanic attack. Seal the hole edge if the panel behind is exposed to spray, because water tracking behind a pad starts corrosion you will not see until the pad comes off. Leave a few millimetres of gap between adjacent pads: butt jointing looks neat on the drawing and produces buckling in service.
Radial cracking from bolt holes is the classic one, from a combination of over-torque, an undersized washer and thermal restraint. The fix is a larger washer face, a controlled torque figure and a clearance hole that allows movement.
Edge chipping happens where a pad meets a steel panel edge with no chamfer, or where the pad is installed with a gap behind it so the edge is unsupported. A flat, fully bedded backing and a radiused edge solve it. Never install over a proud weld or a lump of paint.
Cold flow, sometimes called creep dishing, shows as a dimple under each bolt head and a dished face overall. It is a function of sustained compressive load at temperature and cannot be reversed. Thicker pads and larger washer areas slow it, nothing stops it, which is one reason to keep sustained contact pressure conservative rather than designing to short term compressive strength.
Wear through to the panel is the one that ends berth protection. Once the pad wears through, the rubber or the steel panel is in direct contact with the hull and both the fender and the hull coating start to suffer. That is why inspection interval and wear allowance have to be decided together, and why thickness should never be chosen to the minimum that passes the drawing.
A supplier who receives a proper enquiry quotes a proper product. Send pad dimensions and quantity, thickness with tolerance, resin grade with molecular weight requirement, colour and UV requirement, a drawing or template for the hole pattern including countersink detail, edge treatment, required test reports, and the destination climate and berth type.
Two developments are worth tracking if you are planning berth work. The first is the PIANC 2024 fender guidelines, which have pushed designers to re-examine fender orientation and panel detailing on new installs. The Port of Tampa berth 214 project, for example, revised its original inverted cone arrangement against that guidance before fabrication. Panel orientation changes the load path into the facing pads, so if your project references PIANC 2024, check the pad fixing detail against the final panel geometry rather than the concept drawing.
If you are working through a berth upgrade, a replacement package or a new terminal specification, send the fender panel drawing and the service conditions. We will come back with a thickness and grade recommendation, a drilling template and a material data set you can put in front of the client. For flat fender faces rather than moulded pads, our UHMWPE sheet range covers the same resin grades in sheet form, and the engineering logic in our crane outrigger pad guide applies directly to thickness and bearing pressure decisions.