Static charge in a bulk handling line is not a comfort problem. A dry powder moving at three to five metres per second through a steel chute separates charge faster than any surface can bleed it away, and the plastic liner, being the last thing the material touches, is where that charge collects. If the liner cannot pass it on, the discharge happens at the next earthed object, or through the operator standing at the inspection door.
This guide is written for the person who has to write the purchase specification. It covers what resistivity number to ask for and how to test it, which additive system survives a real duty, what thickness and fixing pattern keep the earth path intact, and the failure modes that actually show up after two winters of service.
Anti-static is a range, not a property. Industry divides plastics into three bands by volume resistivity: conductive below roughly 10^4 ohm-cm, dissipative between 10^6 and 10^9 ohm-cm, and insulating above 10^12 ohm-cm. Neat UHMWPE sits at the far end of the insulating band, around 10^15 to 10^17 ohm-cm, which is why an untreated sheet holds charge like a capacitor plate.
No filled polymer behaves like steel. Even in the conductive band, charge moves slowly and through a resistive network. The purpose of an Anti-static UHMWPE Sheet is to bleed charge at a rate that keeps the surface potential below the ignition or damage threshold, not to conduct current like a busbar. Specifications that ask for “conductive” without a number, a test method and a voltage usually end up with whichever band the supplier had on the shelf.
Two numbers get quoted interchangeably and they are not the same. Surface resistivity describes charge creeping across the face; volume resistivity describes charge passing through the thickness. For a wear liner the volume figure is the material property you are buying, and the surface figure is what an inspector can measure on site.
Surface readings are dominated by contamination and humidity. A coal-dusted face or an oil film will read several decades higher than the same sheet cleaned with isopropanol. That is useful information about the installation, but it is a poor acceptance criterion for the delivered goods. Write the volume resistivity into the purchase order and use surface resistance as the installed check.
State the test conditions or the number means nothing. Resistivity in filled polyethylene is measured at 23 degrees C and 50 percent relative humidity, with a defined electrification time, typically 60 seconds, and a defined voltage, typically 100 V or 500 V. Carbon-loaded compounds are often non-ohmic at high voltage, so a supplier quoting 10^6 ohm without saying at what voltage has told you nothing you can compare. Ask for the voltage, the standard, and the conditioning time in writing.
Carbon black is the workhorse. A percolation network forms somewhere between 8 and 15 percent loading by weight, resistance falls sharply and then flattens, and the effect is permanent because the filler does not migrate. It is the cheapest route, it is unaffected by humidity, and it forces the sheet to be black. Almost every Anti-static UHMWPE Sheet on the market at a competitive price is a carbon black compound.
Carbon nanotubes and carbon fibres reach the dissipative band at one to three percent loading, which preserves most of the impact strength and elongation of the neat resin. The cost is a multiple of carbon black, and dispersion quality decides the result: a poorly dispersed batch has conductive islands in an insulating matrix and can read anywhere between 10^5 and 10^13 depending on where the probe lands. If you buy this route, ask for a resistivity map across the sheet rather than a single coupon value.
Migratory antistatic agents, the surfactant type used in packaging film, should be rejected for liners. They work by absorbing atmospheric moisture into a surface layer, they wash off, they are consumed by abrasion, and they fail in a dry heated plant in January after passing in a humid lab in July. They are appropriate for a bag that lives for six months. They are not appropriate for a chute liner specified for ten years.
If the sheet also has to be flame retardant, you are asking for two additive systems competing for the same volume fraction. Adding a halogen-free FR package usually pushes resistivity up and can drop the fire classification by a sub-class, so the combination has to be tested as a combination. See our notes on flame retardant UHMWPE panels for how the ratings are built up.
Impact strength falls. A carbon black grade in the 10^6 ohm-cm range typically loses a significant share of its notched Charpy value against virgin resin, and the loss is worse at low temperature. In a chute that receives lump material over a 1.5 m drop, that difference is the gap between a liner that dents and a liner that cracks at the fixing holes.
Food and feed contact is the hard stop. Carbon black grades generally cannot demonstrate compliance with EU 10/2011 or FDA food contact requirements unless the grade is specifically certified for it. If the line handles grain, flour, sugar or feed, confirm the certification before the specification is fixed, because no amount of resistivity testing will rescue a non-compliant sheet at an audit.
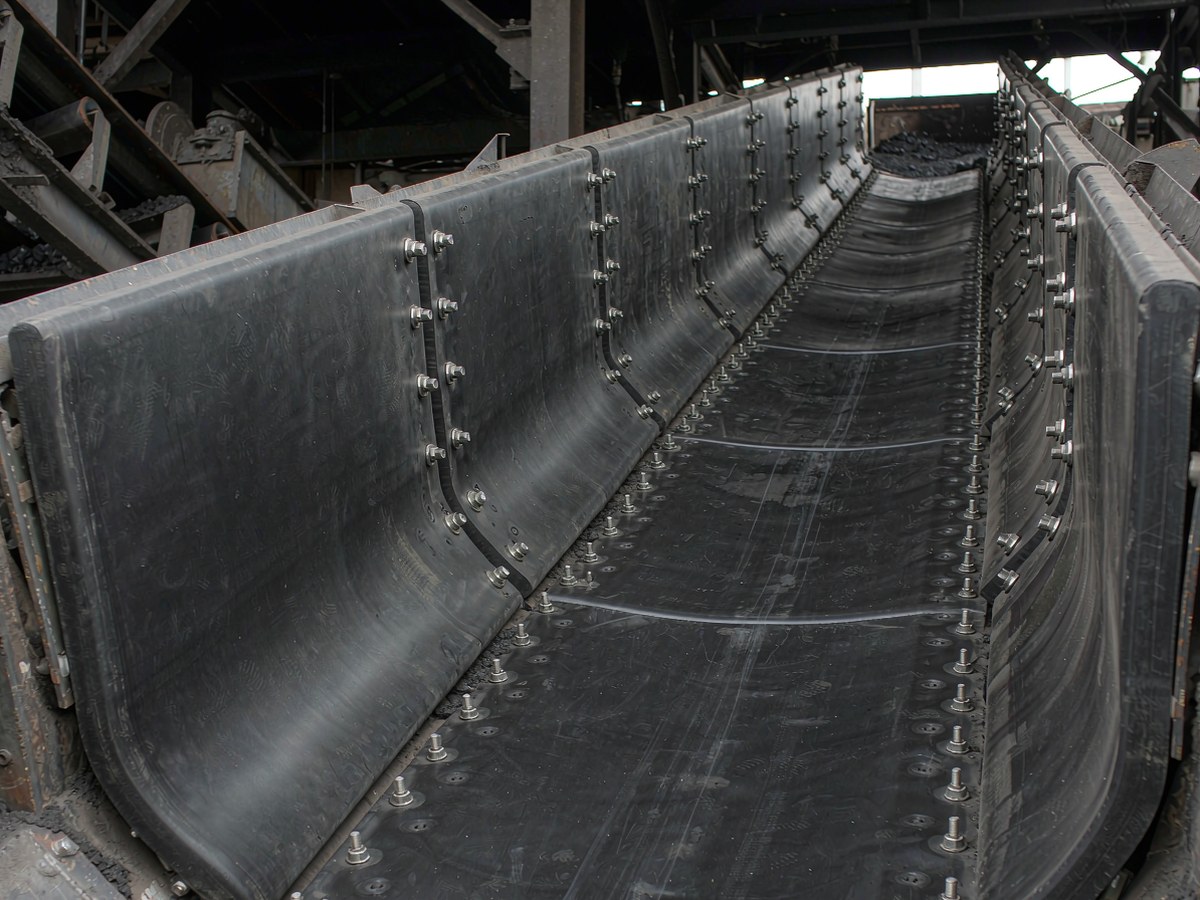
Ten to twelve millimetres suits low angle chutes handling fine powder with a short drop. Fifteen to twenty millimetres covers mixed lump sizes, drop heights above 1.5 m and discharge points where the stream lands on the same strip every shift. Twenty-five millimetres and above belongs in hopper throats, truck beds, dump pockets and primary impact zones where the liner is a wear part first and a static control measure second.
Thickness tolerance is worth writing down. Pressed sheet is commonly quoted at plus or minus five percent, or plus or minus 0.5 mm, whichever is greater; skived sheet holds tighter on thin gauges. This matters more than it sounds, because a panel that runs 1 mm heavy puts the countersunk bolt heads below the wear face and a panel that runs light leaves the heads proud, where the material stream eats them.
An Anti-static UHMWPE Sheet with no path to earth is an insulated plate with a large surface area, and it will hold charge longer than bare steel. The path is short and it is easy to break: sheet to bolt, bolt to structure, structure to plant earth. Break any one link and the specification is decorative.
Fix with stainless A2 or A4 bolts at 300 to 400 mm centres, countersunk where the wear face is exposed, and avoid plastic cap washers or plastic bolt head covers over the fastening points. At panel seams keep fasteners within about 25 to 40 mm of the joint so charge does not have to travel across a long unbonded lap. Where the design uses a metal backing strip, bond the strip to the structure as well.
Surface preparation under the liner is the most commonly missed item. Mill scale, zinc-rich primer and two-pack paint all read in the megohm range and quietly insulate the bolt from the structure. Mask the contact patches before painting, or grind them back at installation, and check the bare steel with a meter before the panel goes on. This costs ten minutes per panel and prevents the most common commissioning argument.
Set a target and test to it. For hazardous dust areas, practice under IEC 60079-32-2 is to keep the resistance from the surface of an installed dissipative lining to earth below 10^6 ohm. Measure with a calibrated megohmmeter at 100 V, probes about 100 mm apart, at least five points per panel after installation, and record ambient humidity with the readings.
Coefficient of linear expansion for UHMWPE runs about 1.5 to 2.0 x 10^-4 per kelvin, roughly ten times steel. A two metre panel therefore grows three to four millimetres over a 10 K swing, and considerably more in an unheated chute.
The workable arrangement is a fixed row at the top, slotted holes at the bottom with a washer that still clamps to bare steel, and a short braided strap or a dedicated bonding bolt where a slot interrupts the contact. The bond only needs to be continuous, not distributed, so one reliable connection per panel is enough if it is inspected.
Black is the natural colour of a carbon black compound. Red, blue and green sheets need a different additive package, and each colour batch needs its own resistivity report rather than a copy of the black one. Blue is often used across a plant as the visual identifier for dissipative material, which is useful on site provided the number behind the colour is real.
The purchase order should carry six lines: base resin and whether recycled content is permitted, additive system and target volume resistivity with test method and voltage, thickness with tolerance and flatness, colour with a sample reference, edge and hole finish, and a per-batch test certificate. Add whether the sheet must be weldable, because the welding rod has to match the compound or the seam becomes an insulating joint in a dissipative panel.
Dust film is the first. Coal, grain and cement dust are insulators; a coated face can climb from 10^7 to 10^12 ohm in a few weeks. The liner is fine, the reading is not, and the fix is a cleaning schedule plus measuring after cleaning rather than before.
Loose fasteners are the second. Under impact and thermal cycling, bolts back out a millimetre or two, contact pressure falls and resistance rises. Add a torque check to the first planned shutdown and again after six months; if the pattern repeats, the fixing centres are too wide for the panel span.
The third is a wrong grade delivered. A black sheet with no conductive filler looks identical to a black sheet with fifteen percent carbon. An incoming test catches it in twenty minutes and is the only defence that does not depend on the supplier’s honesty.
The fourth is a painted or galvanised interface, described above, and it usually appears as a lining that passes in the workshop and fails the first site measurement. The fifth is a moisture-dependent additive in a dry plant, which is why migratory systems should never be accepted for a liner regardless of the test report.
Four checks cover most of the risk. Measure surface resistance on the face that will be installed, at three points, after wiping with isopropanol and allowing the solvent to flash off. Check thickness at five points with a micrometer or a proper gauge, not a tape. Compare colour against the approved sample under daylight. And if the price looks too good, take a shaving and check whether it leaves a continuous carbon trace when heated, which separates a filled compound from a surface-treated one.
It earns its cost in coal and coke handling, grain elevators and silo discharge, powder mixing, FIBC and tanker loading, and any bench where electronic assemblies are handled. It does not earn its cost in wet slurry lines, in food contact duties where carbon black cannot be certified, or in purely mechanical wear applications with no flammable dust and no sensitive electronics. The same money is better spent on thickness and on better fixing.
If you send us the duty – material, particle size, belt speed, drop height, area classification and the resistance target you have to meet – we will come back with a grade, a thickness and a fixing pattern rather than a price list. The anti-static UHMWPE sheet range covers 8 to 300 mm in sheet sizes up to 3000 x 2000 mm, and the same compound is available cut and drilled for UHMWPE chute liners.